If you’ve spent any time in the additive manufacturing (AM) space over the last decade, you know metal printing has evolved from a niche prototyping tool to a production workhorse. As a metal printing supplier, I’ve worked with everything from small aerospace startups printing satellite brackets to large automotive manufacturers scaling brake caliper production, and one question I get asked more than any other is: “How do I optimize my part design for metal printing?” It’s not a trivial question—get it right, and you cut lead times, reduce material waste, and lower production costs by 30% or more, based on our internal project data. Get it wrong, and you’re stuck with scrapped parts, failed prints, and months of rework. Today, I want to pull back the curtain on what we teach our customers and what we’ve learned across hundreds of print jobs to make metal printing work for you. Metal Printing
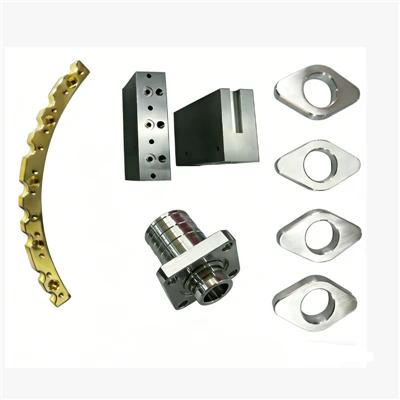
First, let’s ground this in something real. Last year, a medical device customer came to us with a titanium spinal fusion cage they’d been manufacturing via CNC machining. The original part was a solid block of Ti-6Al-4V, 85% of which ended up as scrap chips during milling. They wanted to switch to metal laser powder bed fusion (LPBF)—the most common metal printing technology for production parts—but their initial design sent for testing failed three times in a row. The issue? Overhangs with a steeper angle than our printer’s standard support structures could handle, and thick cross-sections that took 12 hours to print, with severe internal porosity. We reworked the design together in three weeks, cut the material use by 78%, reduced print time to 4.5 hours, and the part passed all FDA biocompatibility and fatigue testing. That’s the kind of optimization that moves the needle, but it starts with ditching the “one-size-fits-all” mindset of traditional manufacturing.
Let’s start with the basics of design for additive manufacturing (DfAM) for metal, and why it’s not just about “making it printable.” Most engineers start with a part designed for CNC or injection molding, then try to tweak it for metal printing—but that’s backwards. Metal printing builds parts layer by layer, melting or fusing fine metal powder with a high-powered laser or electron beam, so the rules are different. The first non-negotiable rule: eliminate unnecessary material. In CNC, adding thickness to a wall is easy to hide, but in metal printing, every extra cubic centimeter of material means more powder, longer print time, and higher risk of thermal stress. That’s why topology optimization is such a powerful tool here—but it’s not a plug-and-play fix. We’ve seen teams run topology optimization on a part only to get a design with thin, delicate walls that warp during printing, because the algorithm doesn’t account for real printer constraints.
Thermal stress is the biggest hidden enemy of metal printing, and it’s where most first-time optimizations go wrong. When a laser melts a layer of powder, it heats the surrounding material to 1,000+ degrees Celsius, then it cools in seconds. That rapid heating and cooling causes the part to expand and contract unevenly, leading to warping, cracking, or even the part pulling free from the build plate mid-print. The fix here is twofold: first, design parts to minimize sudden changes in cross-sectional area, and second, use support structures only where you absolutely need them. Supports are the most hated part of metal printing—they’re made of the same metal as your part, they have to be machined or sanded off post-print, and they can add 20% to 50% to your post-processing time.
Take overhangs, for example. A 45-degree overhang is manageable with thin, low-volume supports, but anything below 30 degrees is a problem—even the most advanced printers can’t melt powder accurately enough to support the overhang of the new layer without the extra structure. That doesn’t mean you have to redesign every sloped surface to be steeper, though. We work with customers to split overhangs into smaller segments, add small dimples or fillets at the base of overhangs to distribute heat, or even use a hybrid design where a small, temporary internal structure is printed only to support that area, then dissolved or machined away post-print. For that spinal fusion cage I mentioned earlier, we turned a 22-degree overhang into four 10-degree segments, each supported with a minimal amount of lattice structure that we could remove in 15 minutes of machining, no extra work.
Next, let’s talk about wall thickness. This is a common mistake among new metal printer users. A lot of engineers assume thicker walls are stronger, but in metal printing, walls that are too thick develop internal porosity because the laser can’t fully melt the core of the material. For Ti-6Al-4V, the sweet spot is between 0.8mm and 2.0mm for most production parts. Go thinner than 0.8mm, and the walls are too delicate to resist thermal stress and will warp. Go thicker than 2.0mm, and you’re wasting material and print time, with higher risk of defects. We had an aerospace customer recently who designed a bracket with 3.5mm walls because that’s what they used for CNC. When we ran a test print, the core of the wall was so porous that it failed a torque test at 40% of the required load. We trimmed the walls to 1.5mm, added internal lattice ribbing to boost strength, and the part passed the torque test at 120% of the required load, using 40% less material. Lattice structures are another underutilized optimization tool, by the way—they add strength without the weight of solid material, which is perfect for aerospace, automotive, and medical parts where weight is a critical factor.
Print orientation is another piece of the optimization puzzle that’s often overlooked. The way you orient a part on the build plate has a massive impact on print time, support use, and part quality. A part oriented vertically might have less support, but it could have more surface area exposed to the laser, leading to higher residual stress. Orienting it horizontally might reduce stress, but it could require more supports and take longer to print. There’s no one right answer here, which is why we always do a pre-print analysis for our customers, calculating three or four different orientation scenarios to compare. For example, we worked with a consumer electronics client who needed a thin, complex heat sink for a 5G router. They initially oriented it vertically, which required supports for 12 fins, added 3 hours of print time, and the fins had slight surface roughness that hurt heat dissipation. We reoriented it at a 30-degree angle, which only required supports for two of the fins, cut print time by 2.5 hours, and the surface finish was smooth enough to boost heat dissipation by 18%.
Surface finish is another area where optimization matters, depending on your end use. For parts that need to be polished or have tight tolerances, you might design extra material into high-tolerance areas to account for post-processing. For example, if you need a bearing surface with a tolerance of ±0.05mm, you can add 0.2mm of stock to that area, then machine it down after printing, instead of trying to print the exact tolerance. That’s far more reliable than trying to get a perfect finish on a thin, complex surface in the printer, which would add days of rework. On the other hand, if you don’t need a polished surface—like a structural bracket that’s going to be coated—you can reduce print resolution slightly to cut down on print time, since lower resolution prints are faster and use less powder, and the coating will hide any slight surface texture.
Material selection shouldn’t be an afterthought either. A lot of customers come to us wanting to use a “standard” material like Ti-6Al-4V, but there are dozens of metal alloys optimized for different printing processes. For example, maraging steel is great for high-strength tools and dies, while aluminum AlSi10Mg is perfect for heat-intensive parts because it has excellent thermal conductivity. We recently had a customer who was printing an engine component using 17-4 PH stainless steel, which required high heat treatment to reduce residual stress. We switched them to a custom alloy blend we use for high-temperature applications, which cut the heat treatment time in half and reduced part warpage by 90%. It’s important to note that not all alloys are printable—some have higher thermal expansion rates that make them prone to cracking, so working with a supplier who understands material-specific constraints is key.
Quality control is also part of the design optimization process, even if it seems like a post-print step. You can design the most perfect part in the world, but if it can’t be inspected easily, you’ll run into issues down the line. For example, designing internal cavities with easy access for CT scanning or ultrasound testing will help you catch defects early, instead of finding out after you’ve printed 100 parts that you can’t inspect the interior. We always recommend adding small inspection ports or reference features to parts designed for metal printing, which take almost no extra material but save hundreds or thousands of dollars in rework and compliance testing.
Now, let’s address the common myths that hold people back from optimizing their metal printing designs. The first myth: DfAM is only for complex, custom parts. No—we’ve optimized mass-produced parts like automotive brake calipers, with over 10,000 units printed per year, cutting costs by 45% compared to CNC machining. The second myth: You need expensive software to optimize your design. While topology optimization software can help, a lot of basic optimizations—trimming excess material, adjusting wall thickness, reducing overhangs—can be done with a simple design review, no fancy tools required. The third myth: Optimized parts are less strong. As I showed with that bracket example, optimized parts can be stronger and lighter than traditionally manufactured parts, because you’re only using material where it’s needed.
Over the years, I’ve seen companies that treat metal printing as just another way to make parts, and companies that leverage it to redesign their products entirely. The medical device client that switched from solid titanium cages to lattice-filled ones reduced patient recovery time by 20%. The aerospace client that optimized their satellite brackets cut the total weight of the satellite by 12%, which translates to thousands of dollars in launch costs. The automotive client that optimized their brake calipers increased their torque capacity by 30%. These aren’t small wins—they’re game-changers for entire industries.
At the end of the day, optimizing design for metal printing isn’t a one-time task. It’s an iterative process that starts when you first sketch out your part, not after you hit print. If you’re new to metal printing, or if you’ve had a few bad experiences with scrapped parts or high costs, the best next step is to work with a supplier that understands both the technical side of metal printing and the real-world needs of your industry. We don’t just send a customer a quote and a part—we walk through their design, test different iterations, and adjust every detail to make sure the final part is printable, cost-effective, and meets all their performance requirements.
If you’re ready to turn your part from a CAD file into a high-quality, production-ready metal printed component, we’re here to help. Whether you’re designing a prototype, scaling production, or rethinking a part that’s been made the same way for decades, we can work with you to optimize every step of the process. Reach out to discuss your project and we can walk through how metal printing can deliver value for your specific needs.
SLS Printing References
- Gibson, I., Rosen, D. W., & Stucker, B. (2015). Additive Manufacturing Technologies: 3D Printing, Rapid Prototyping, and Direct Digital Manufacturing. Springer.
- Lee, J. H., et al. (2020). Design for additive manufacturing: A review of process constraints, design strategies, and tools. International Journal of Precision Engineering and Manufacturing-Green Technology.
- Murr, L. E., et al. (2012). Metal fabrication by additive manufacturing using laser and electron beam melting technologies. Journal of Materials Science & Technology.
- Tiwari, A., et al. (2022). Thermal stress mitigation in laser powder bed fusion additive manufacturing: A review of design and process optimization strategies. Additive Manufacturing.
Dongguan Xinchuan Precision Manufacturing Co., Ltd.
As one of the most professional metal printing manufacturers and suppliers in China, we offer a quick lead time for customized orders. Please feel free to buy precision metal printing made in China here from our factory. Contact us for quotation.
Address: #16 Gangjian Road, Changping Town, Dongguan City, Guangdong, China. 523000
E-mail: FreeQuote@xcprecision.com
WebSite: https://www.xcprecisions.com/
